Let me start with a true story that has circulated in manufacturing circles for years.
A Chinese equipment maker supplied a German customer. The equipment arrived, failed acceptance, and was returned in full. The inspection puzzled the Chinese engineers — every single bolt was tight, not one loose.
The German reply: "You tightened the bolts `all the way down` — but our standard is `three turns forward, half a turn back`."
Three turns, then half a turn back? Superfluous? Not at all.
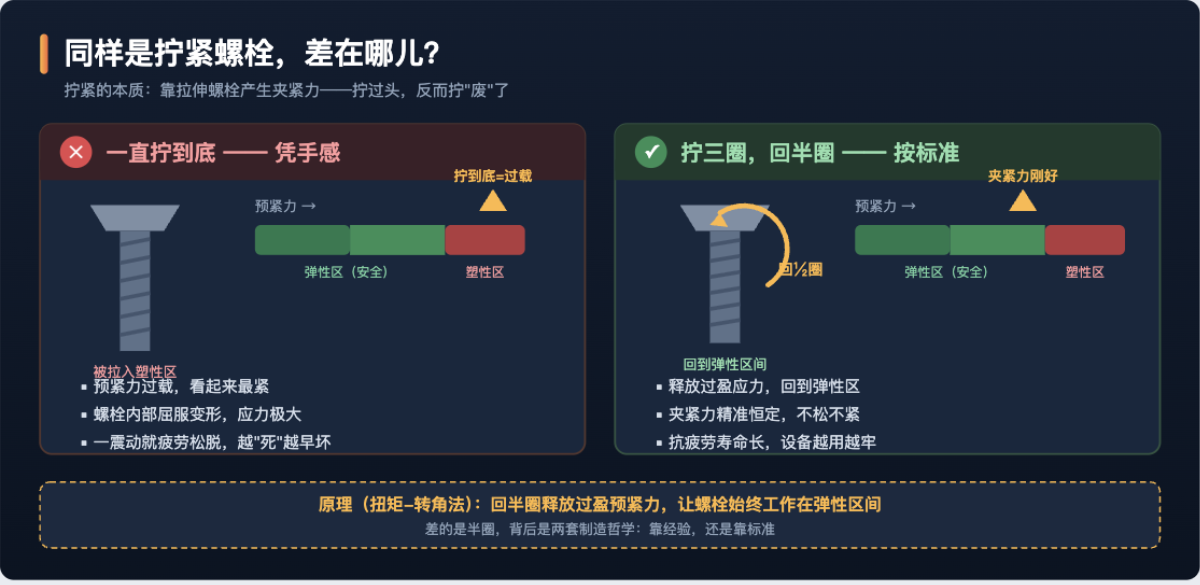
1. What does the half turn give back?<br>Tightening a bolt works by stretching it to create clamping force, gripping two parts together.
Tighten all the way down and the bolt enters the "plastic zone" — the material is stretched into slight yield. It looks tightest, but the preload is overloaded and internal stress extreme; with vibration and thermal cycling, fatigue failure risk multiplies. The tighter it is "dead," the earlier it fails.
Three turns then half a turn back returns the bolt to the "elastic zone" — that half turn of release sheds exactly the excess stress, landing clamping force within design range: not loose, not tight, durable and constant.
<img src="../assets/img/uploads/mw76ihu0339b84.png" alt="" style="display:inline-block;max-width:100%;border-radius:10px;margin:8px 0;vertical-align:middle"><br>Same bolt, same wrench: one tightens by feel "as far as it will go," the other to standard "just right." The difference is half a turn — <strong>behind it stand two philosophies of manufacturing: experience versus standard.</strong>
The strength of German manufacturing lies not in stronger arms but in a validated standard behind every motion. This is the first principle of lean production — <strong>turning the master's touch into standards everyone can execute, replicate and audit.</strong>
2. Three real slices from the shop floor<br>In years of lean consulting across Shandong manufacturers, I have seen too much "all-the-way-down" effort — wrong direction, more waste.
Slice one: orders doubled, capacity stood still. A manufacturer's orders tripled in three years while output idled. The boss ordered overtime — ten hours a day, output unmoved. Diagnosis found the whole line's yield capped by one bottleneck operation; the harder the others ran, the more WIP piled in front of it. Three focused improvements later, without adding a single machine, capacity rose 40% and overtime was cancelled first.
Slice two: the more they repaired, the worse it got. A maintenance crew firefighting daily, breakdowns constant. The repair log showed the same failure on the same machine seven times in a year — always treating the symptom, never the cause. With TPM autonomous maintenance and ten minutes of daily inspection by operators, downtime fell by more than half; the crew moved from firefighting to fire prevention.
Slice three: messy floor, low efficiency. A food company needed ten minutes to find a tool, ran FIFO on memory, fought recurring oil stains. After 6S fixed-location management and visual control, retrieval dropped to ten seconds. Shop-floor management is the foundation of a factory's efficiency.
3. The lean map: seven wastes<br>Everything lean production does comes down to one thing: <strong>find and eliminate every action that creates no value.</strong>
<img src="../assets/img/uploads/mw76irw3422459.png" alt="" style="display:inline-block;max-width:100%;border-radius:10px;margin:8px 0;vertical-align:middle"><br>Check your own plant against the list — most factories tick all seven. <strong>Waste is not the employees' fault; the system makes waste look normal.</strong>
4. How to start: a four-step path<br>Most failed lean campaigns die of "a hundred days of all-out war" on day one. Ours is four steps:
<img src="../assets/img/uploads/mw76iynw71be02.png" alt="" style="display:inline-block;max-width:100%;border-radius:10px;margin:8px 0;vertical-align:middle"><br>Step one, gemba diagnosis. Establish where bottlenecks, waste and losses are and what they cost — our habit is to do this step free of charge; the data speaks, and the owner decides whether it is worth doing.
Step two, bottleneck breakthrough. No shotgun: concentrate on the one or two points of greatest leverage — usually visible within 45 days, so everyone sees that lean works.
Step three, standard work. Write the gains into standard work sheets (like "three turns, half a turn back") and lock them with visual boards — so improvements survive personnel changes.
Step four, continuous improvement. Grow the company's own improvement backbone and a proposal system — improvement shifts from "the consultant's job" to "everyone's daily job."
5. Seven questions: how heavy is your factory's waste?<br>WIP stacked between operations, blocking aisles and tying up cash<br>Material handling routes growing longer every revision, handlers always short<br>People waiting for materials, machines waiting for repair, work waiting for batches<br>The same quality problem recurring, treated at the surface only<br>Overtime rising year after year with per-capita output flat<br>Repair only after breakdown, the maintenance crew firefighting daily<br>Finding a tool or material on the floor takes more than a minute
Closing words<br>Shandong manufacturers have competed on cost and capacity for decades; the next decade competes on refined efficiency and quality. Lean is not a cost-cutting campaign — it makes every yuan of input grow on value customers pay for.
From "all the way down" to "half a turn back": that half turn is the distance between an ordinary factory and an excellent one.
Author: Jing Yong | Founder, Qingdao Lizheng Enterprise Management Consulting Co., Ltd.
With 20+ years in management consulting and 500+ enterprises served across power, steel, chemicals, pharmaceuticals, rail transit and equipment manufacturing — over 30 industries.
Website: https://www.startermc.com | Hotline: 138-6397-8878